

Spraying Application Case of AT600SP Zircon‑Flour Coating on Wind Power Hub Castings
2026-09-07 10:37Wind power hubs are basically ductile iron castings that are heavy duty, weighing in one piece of about 29 tons, with maximum wall thickness of 120 mm. The very long pouring cycle puts great demand for the temperature stability and capacity of the coating to form of the foundry coating at high temperature. Brushing the coating in the traditional way has many issues such as low productivity and the brush marks on the coating which are a bit annoying. Cleaning work after the casting is heavy, which limits the ability of foundories to deliver mass production of wind‑power castings.
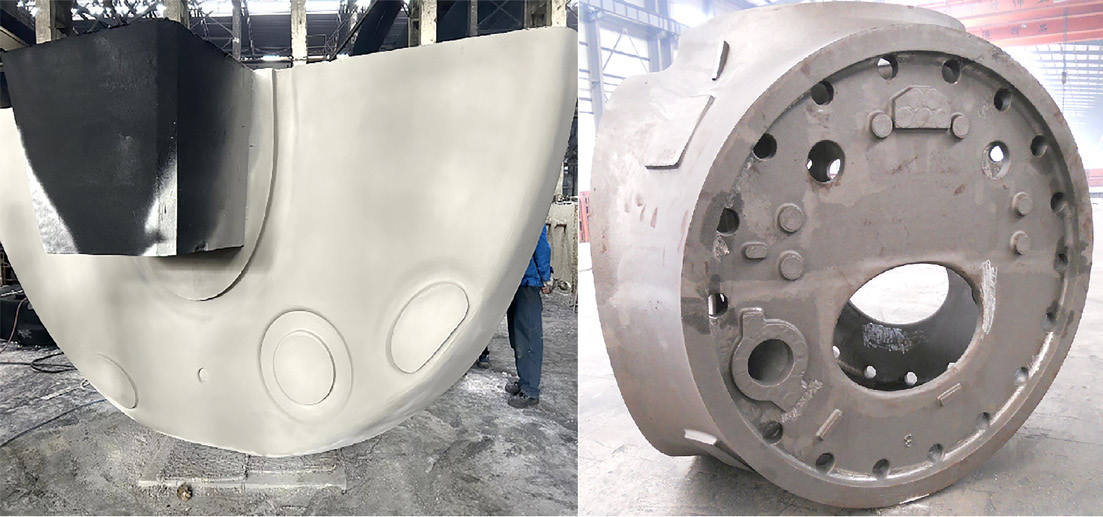
Under furan resin sand conditions the application of zircon‑flour coating XINDAAT600SP is done by airless spraying. Coating spraying has helped to improve coating efficiency, coat with protective function, even in the same thickness, smoothness of the surface, and the improvement of the quality on the surface of the wind power hub casting are among the results.
Ⅰ、Product, Casting and Production Process Parameters
Technical Specifications of AT600SP:
| Coating Appearance | Original Baume Degree (Be) | Original Density (g/cm³) | 2‑hour Suspension Rate (%) | 24‑hour Suspension Rate (%) | Gas Evolution (ml/g) | Coating Abrasion Resistance (<g,64r) |
|---|---|---|---|---|---|---|
| White paste | ≥120 | 1.7‑2.2 | ≥98 | ≥95 | <18 | 0.4 |
Casting Information:
| Casting Name | Hub |
| Material | QT350‑22AL Ductile Iron |
| Application Field | Wind‑power Equipment Casting |
| Melting Equipment | Medium‑frequency Induction Furnace |
| Total Pouring Weight | 33T |
| Net Casting Weight | 29T |
| Pouring Time | 291s |
| Pouring Temperature | 1360℃ |
| Mold Sand Type | Furan Resin Bonded Sand |
| Core Sand Type | Furan Resin Bonded Sand |
| Average Wall Thickness | 80mm |
| Maximum Wall Thickness | 120mm |
| Original Production Painpoints | Low efficiency of manual brushing, obvious brush marks, difficulty in obtaining coatings with uniform thickness and smooth finish |
Production Process & Application Details:
Coating Application Method | Spraying Passes | Working Baume Degree | Spraying Technique | Drying Method | Coating Thickness | Surface Strength of Coating | Surface Strength of Coating |
|---|---|---|---|---|---|---|---|
| Spraying | 2 passes | 72 Be° | Airless Spraying | Flame Drying | 0.6‑0.8mm | High strength | Smooth surface, free of cracks and brush marks |
Ⅱ、Core Advantages of AT600SP Zircon‑Flour Coating
Excellent suspension performance for stable storage and on‑site application
The 2‑hour suspension rate reaches ≥98% and the 24‑hour suspension rate ≥95%. The coating avoids delamination and sedimentation during storage and maintains stable slurry properties for continuous spraying operation.
Low gas evolution to minimize porosity risks
The gas evolution value is less than 18 ml/g. Controlled gas release during long‑term high‑temperature pouring for heavy‑section wind‑power castings effectively reduces casting porosity defects.
Outstanding abrasion resistance for reliable high‑temperature protection
With an abrasion resistance value of 0.4, the high‑strength coating resists erosion by high‑temperature molten iron and forms an effective barrier between liquid metal and sand mould.
Compatible with airless spraying for greatly improved productivity
The paste‑form coating can be directly used for airless spraying after dilution to the working Baume degree. Spraying efficiency doubles compared with manual brushing, suitable for mass production of large 1000T‑1500T wind‑power castings.
Ⅲ、On‑site Application and Result Analysis
Airless spraying was adopted with two spraying passes. The coating thickness was controlled at 0.6‑0.8 mm and cured by flame drying.
Exceptional appearance of coating after finishing: The coating is not only smooth and flat but also without brush marks and cracks. The uniform thickness is well controlled.
Significantly enhanced productivity: In comparison to the traditional brushing, the spraying increases the productivity by a factor of two. One operator only can manage the coating work for large 1000‑1500‑ton casting of wind‑power.
Complete coating stripping after pouring: The whole coating peels off only after cooling and thus casting surfaces are smooth.
Getting rid of burn-on defects: There is no penetration of metal through the casting which makes the grinding and cleaning workload to decrease considerably. This in effect reduces the time and money spent on the post- processing.
Xinda AT600SP zircon‑flour coating is a special preparation intended to be used for the heavy‑wall ductile iron wind‑power castings. Automatic airless spray is an excellent system with which AT600SP Zircon Flour coating can be used to strike a balance between the high-efficient construction method and better anti- burn-on properties. This is particularly favored for the mass-produced heavy‑casting parts of wind power including hubs, bed frame and gear box casing.